Wire Cut EDM Machines Information With Electrical Discharge Machining and Manufacturing Insights
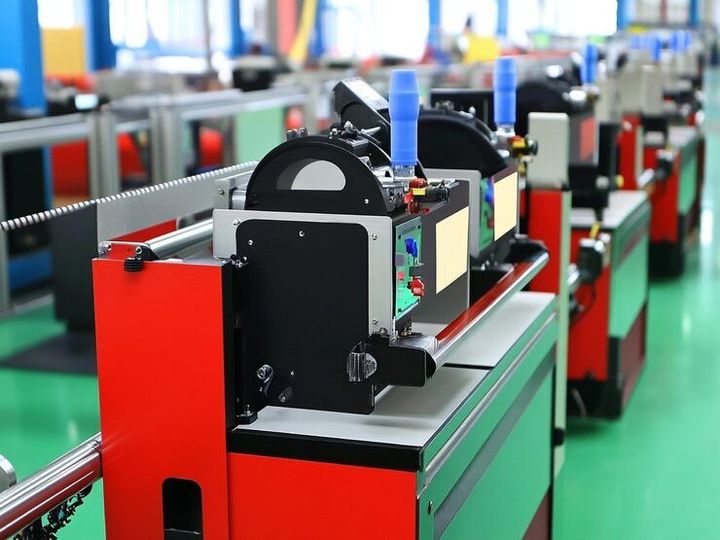
Wire Cut EDM Machines are precision manufacturing systems that use electrical discharge machining to cut electrically conductive materials into complex shapes.
EDM stands for Electrical Discharge Machining, a process in which controlled electrical sparks remove tiny amounts of material without requiring a conventional cutting tool to press directly against the workpiece. This technology is particularly useful for producing intricate profiles, narrow slots, sharp internal corners, and detailed components.
The development of electrical discharge machining addressed manufacturing challenges associated with cutting hard metals and producing geometries that are difficult to achieve through traditional machining. Wire EDM evolved as a specialized method that uses a thin, electrically conductive wire as an electrode. The wire follows a programmed path while electrical discharges gradually remove material from the workpiece.
Modern Wire Cut EDM Machines are used in toolmaking, automotive manufacturing, aerospace production, electronics, medical equipment manufacturing, and precision engineering. Their operation combines electrical energy, computer numerical control (CNC), controlled wire movement, and dielectric fluid management. Understanding these systems helps explain how manufacturers produce accurate metal components for different industrial applications.
How Wire Cut Electrical Discharge Machining Works
A wire EDM system typically contains a power supply, wire feed mechanism, CNC controller, worktable, dielectric fluid system, and a tank that holds or surrounds the workpiece. The machine guides a thin wire, commonly made from brass or another conductive material, along a predetermined cutting path.
During operation, a small gap separates the wire from the conductive workpiece. Electrical pulses generate sparks across this gap, creating localized heat that melts or vaporizes tiny quantities of material. The dielectric fluid helps control the electrical discharge, cool the cutting area, and remove debris.
The wire does not normally make direct mechanical contact with the workpiece during cutting. This reduces cutting forces and allows the production of delicate features that might be difficult to machine using conventional milling or sawing methods.
Main Components of Wire EDM Equipment
The principal components perform different functions within the machining process.
CNC controller: Interprets programmed instructions and coordinates the movement of the wire and worktable.
Wire electrode: Conducts electrical energy to generate the discharges that remove material.
Power supply: Controls the electrical pulses used during machining.
Dielectric system: Circulates and filters the fluid surrounding the cutting area.
Wire tension mechanism: Maintains appropriate wire tension to support dimensional accuracy.
Servo control system: Regulates the gap between the wire and the workpiece.
Automatic wire threading system: Feeds and threads the wire through the workpiece when supported by the machine.
Together, these components determine cutting stability, surface quality, machining speed, and dimensional accuracy.
Importance
Wire Cut EDM Machines are important because many manufacturing applications require precise shapes in hard conductive materials. Conventional cutting tools can experience significant wear when machining hardened steel, tool steel, and certain conductive alloys. Wire EDM can process these materials without depending on a conventional cutting edge to remove the material.
The technology also supports the production of intricate parts with narrow openings, complex outlines, and fine internal features. Since the process applies relatively little mechanical force to the workpiece, it can be useful for thin components and carefully designed tooling.
Industries That Use Wire EDM Technology
Several manufacturing sectors depend on electrical discharge machining for specialized components.
Tool and die manufacturing: Produces stamping dies, punches, forming tools, and precision inserts.
Automotive manufacturing: Supports the production of injection tooling, precision fixtures, and specialized metal components.
Aerospace engineering: Helps manufacture intricate conductive components and tooling used in demanding production environments.
Electronics: Creates precision contacts, connector components, and small tooling features.
Medical equipment manufacturing: Supports the production of selected precision instruments and component tooling.
General engineering: Produces prototype parts, replacement components, and complex profiles for industrial equipment.
The suitability of Wire Cut EDM Machines depends on the workpiece material, geometry, required tolerance, production volume, and surface finish requirements.
Wire EDM Compared With Conventional Machining
Wire EDM differs from milling, turning, and sawing in its material-removal mechanism. Conventional machining uses a cutting tool that mechanically removes material, whereas EDM uses controlled electrical discharges. This distinction influences which applications are suitable for each method.
Manufacturing factor | Wire Cut EDM | Conventional machining |
|---|---|---|
Material requirement | Electrically conductive materials | Depends on the tool and machining process |
Material removal | Electrical discharges | Mechanical cutting |
Cutting force | Very low mechanical cutting force | Cutting forces are present |
Complex profiles | Suitable for intricate two-dimensional and tapered profiles | Depends on tool access and geometry |
Tool contact | No normal direct cutting contact | Tool contacts or engages the workpiece |
Surface characteristics | Can produce fine finishes with suitable settings | Depends on the tool, material, and cutting conditions |
Typical applications | Dies, precision inserts, complex profiles | Shafts, housings, holes, and general components |
Limitations and Operating Challenges
Wire EDM has several limitations that influence its use. The workpiece must be electrically conductive, so ordinary plastics, glass, and most nonconductive ceramics cannot be processed directly using conventional wire EDM.
Material removal may also be slower than conventional machining when large volumes of material must be removed. The wire is consumed during operation, and unstable discharge conditions can cause wire breakage or dimensional errors.
Other considerations include electricity consumption, dielectric fluid maintenance, wire quality, electrode selection, and the need for trained operators. The process may also produce a heat-affected layer on the machined surface, making additional finishing necessary for certain applications.
Recent Updates
Developments in Wire Cut EDM Machines increasingly focus on automation, digital control, process monitoring, and improved production consistency. Across the 2024–2026 period, these areas reflect broader manufacturing trends rather than a single universal technological change.
Automation and Smart Manufacturing
Modern EDM systems increasingly incorporate automatic wire threading, programmable machining sequences, and improved recovery functions. Automatic threading can reduce manual intervention when a wire breaks or when multiple cutting operations must be completed.
Integration with computer-aided manufacturing systems also allows engineers to transfer part geometry and machining instructions into CNC-controlled production workflows. These capabilities support repeatable operations and improve coordination between design and manufacturing teams.
Improved Accuracy and Surface Quality
Manufacturers continue to develop more precise motion control, electrical pulse management, and wire tension regulation. These systems help maintain a stable discharge gap and limit deviations during intricate cuts.
Multiple cutting passes are often used when a component requires improved dimensional accuracy or a smoother surface. An initial rough cut removes most of the material, while subsequent skim cuts refine the geometry and reduce surface irregularities.
Data Monitoring and Energy Management
Digital monitoring can help operators identify changes in machining conditions, wire consumption, fluid quality, and equipment performance. Some systems provide alarms or diagnostic information that helps identify operating problems before they interrupt a production cycle.
Energy efficiency is another consideration for manufacturing facilities. Optimizing pulse settings, reducing unnecessary machine idle time, and maintaining dielectric filtration can support more controlled resource use. Actual improvements depend on the machine design, workpiece, operating settings, and maintenance practices.
Laws or Policies
Wire Cut EDM Machines are affected by workplace safety requirements, electrical equipment standards, environmental controls, and manufacturing quality procedures. The precise requirements depend on the country, the industry, and the facility in which the equipment operates.
Workplace and Electrical Safety
Industrial facilities generally need procedures that address electrical hazards, moving machinery, fire risks, fluid handling, and maintenance activities. Operators must understand machine-specific safety instructions and the correct procedures for isolating electrical power before maintenance.
Relevant safety measures may include:
Electrical protection and appropriate grounding.
Guards, interlocks, and emergency-stop systems.
Safe handling and storage of wire electrodes.
Procedures for cleaning, filtration, and dielectric fluid replacement.
Training for machine operation and maintenance.
Controls for fire hazards associated with combustible materials or unsuitable fluids.
Applicable occupational safety rules and electrical equipment requirements should be identified for the facility's jurisdiction.
Environmental and Quality Requirements
Dielectric fluids, filtration residues, and machining waste may require controlled handling. Facilities should follow applicable environmental requirements for storage, disposal, and the management of contaminated materials.
Manufacturers producing components for regulated industries may also need documented inspection procedures, calibration records, material traceability, and process validation. International quality management frameworks, including ISO 9001, can provide a structure for consistent production and quality control. Certification requirements depend on customer contracts, industry expectations, and applicable regulations.
Tools and Resources
A combination of engineering software, measurement equipment, and maintenance documentation supports the effective use of Wire Cut EDM Machines. The appropriate resources depend on component complexity, production requirements, and operator experience.
CAD and CAM Software
Computer-aided design (CAD) software is used to create component geometry and technical drawings. Computer-aided manufacturing (CAM) software helps convert design information into toolpaths and machining instructions compatible with the selected CNC system.
Important functions include geometry verification, path simulation, cutting sequence planning, and collision checking where applicable. Software compatibility should be confirmed before transferring programs to a machine.
Measurement and Inspection Equipment
Dimensional inspection verifies whether the finished component meets its drawing specifications. Common equipment includes coordinate measuring machines, optical measurement systems, micrometers, and precision gauges.
Surface roughness testers can assess the texture of machined surfaces. The choice of inspection method depends on the required tolerance, feature size, surface characteristics, and quality documentation requirements.
Maintenance and Process Planning Tools
Maintenance records help track wire consumption, filter changes, dielectric condition, machine alarms, and scheduled inspections. Machining parameter tables supplied by equipment manufacturers can help operators select initial settings for different materials and workpiece thicknesses.
The following table summarizes common resources and their uses.
Tool or resource | Primary purpose | Typical application |
|---|---|---|
CAD software | Create component geometry | Part design and drawing preparation |
CAM software | Generate machining paths | CNC program preparation |
CNC simulation | Review machining sequences | Error detection before production |
Coordinate measuring machine | Inspect component dimensions | Precision quality control |
Surface roughness tester | Measure surface texture | Finish verification |
Dielectric filtration equipment | Maintain fluid cleanliness | Stable machining conditions |
Maintenance log | Record inspections and faults | Equipment reliability monitoring |
These resources work together to support production planning, dimensional verification, and process consistency.
FAQs
What are Wire Cut EDM Machines used for?
Wire Cut EDM Machines are used to produce precision shapes in electrically conductive materials. Common applications include stamping dies, punches, tooling inserts, intricate metal profiles, and specialized engineering components.
How does electrical discharge machining cut metal?
Electrical discharge machining removes material through controlled electrical sparks between a wire electrode and a conductive workpiece. The sparks generate localized heat that removes small quantities of material, while dielectric fluid helps control the process.
Which materials can Wire Cut EDM Machines process?
These machines can process electrically conductive materials such as tool steel, hardened steel, stainless steel, copper, brass, and certain conductive alloys. Suitability depends on the machine, material properties, workpiece dimensions, and machining requirements.
What is the difference between wire EDM and CNC milling?
Wire EDM removes material through electrical discharges, whereas CNC milling uses a rotating cutting tool. Wire EDM is particularly useful for intricate profiles in conductive materials, while milling can process a wider range of geometries and materials depending on the tooling.
What factors affect wire EDM accuracy?
Accuracy depends on wire tension, electrical settings, material thickness, thermal conditions, machine calibration, workpiece stability, and CNC control. Wire quality, dielectric fluid condition, and the number of finishing passes can also influence the final result.
Conclusion
Wire Cut EDM Machines use controlled electrical discharges to manufacture intricate components from electrically conductive materials. Their applications include toolmaking, automotive production, electronics, aerospace engineering, and precision manufacturing. Automation, improved CNC controls, digital monitoring, and process optimization continue to shape developments in the technology. Understanding machine capabilities, safety requirements, inspection methods, and operating limitations provides a foundation for evaluating wire EDM within modern manufacturing systems.
You May Also Like