Explore Industrial Quality Control Systems With Modern Testing and Monitoring Technology
Industrial quality control systems are organized methods used to inspect materials, measure production results, identify defects, and monitor whether manufactured products meet defined specifications.
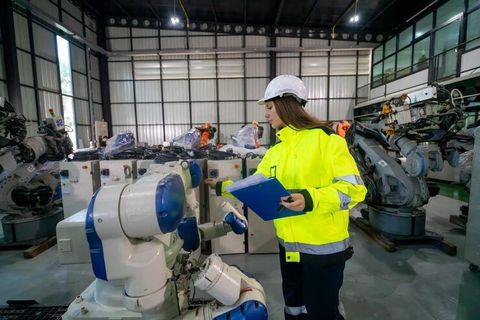
These systems combine inspection equipment, testing instruments, sensors, software, procedures, and trained personnel. Modern quality control increasingly connects physical testing with automated data collection and digital monitoring.
The development of industrial quality control began with the need for consistent manufacturing results. Early factories relied heavily on visual inspection and manual measurement. As production became more complex, manufacturers introduced specialized gauges, testing instruments, statistical methods, and inspection procedures to identify variations during production.
Today, industrial quality control systems can operate at several stages. Materials can be inspected when they enter a facility, products can be checked during production, and finished items can undergo final testing before entering storage or distribution. The objective is to identify differences from established specifications and provide information for corrective action.
Modern testing and monitoring technology has expanded the capabilities of these systems. Cameras can inspect surfaces, sensors can measure process conditions, and automated instruments can record dimensional or physical characteristics. Software can organize the resulting information and make trends easier to examine.
Main Elements of Industrial Quality Control
A quality control system usually contains several connected elements. Inspection equipment examines products, while testing instruments measure specific characteristics. Data systems store measurements and inspection results for later analysis.
Common elements include:
Dimensional measurement equipment
Vision inspection cameras
Material testing instruments
Temperature and pressure sensors
Weight measurement systems
Surface inspection equipment
Automated testing stations
Data collection software
Statistical analysis tools
Inspection documentation
The exact combination depends on the industry. Metal production, electronics, automotive manufacturing, food processing, plastics, pharmaceuticals, and construction materials can require very different testing methods.
Testing and Inspection Methods
Quality control can involve destructive and non-destructive testing. Destructive testing examines a sample by applying forces or conditions that may alter or damage it. Non-destructive testing examines characteristics without intentionally destroying the inspected item.
Examples include dimensional inspection, hardness testing, tensile testing, visual inspection, ultrasonic testing, surface analysis, electrical testing, and imaging-based inspection. Each method has a specific purpose and requires suitable equipment and procedures.
Importance
Industrial quality control systems matter because manufacturing processes naturally experience variation. Raw materials can differ, machines can change condition, environmental conditions can shift, and production settings can drift over time.
Monitoring these changes can help manufacturers identify problems before they become widespread. Quality control also provides records that can be used to investigate recurring defects, compare production batches, and understand process behavior.
Who Uses Quality Control Systems?
Quality control technology affects many industrial groups, including manufacturers, laboratory teams, production personnel, maintenance teams, engineers, inspectors, warehouse personnel, and organizations responsible for regulatory compliance.
Consumers are also indirectly affected because quality control can influence the consistency and safety characteristics of products used in everyday life. The specific requirements depend on the product and industry.
Process Monitoring
Traditional inspection often focused on the finished product. Modern systems increasingly monitor the manufacturing process itself.
Sensors can continuously measure variables such as:
Temperature
Pressure
Humidity
Flow rate
Vibration
Speed
Weight
Electrical characteristics
Machine position
When measurements move outside defined limits, the control system can generate an alert or initiate a predefined response. The response depends on how the production system has been designed.
Traceability and Documentation
Quality control also involves traceability. A manufacturing record may connect a product or production batch with raw materials, machine settings, inspection results, operator records, and equipment information.
Digital records can make it easier to locate information during an investigation. They can also help identify patterns across multiple production runs.
Recent Updates
From 2024 through 2026, industrial quality control has continued moving toward automated inspection, connected sensors, machine vision, artificial intelligence-assisted analysis, digital records, and integrated production monitoring. The broader direction is toward collecting quality information closer to the point where production occurs.
Machine Vision Inspection
Machine vision has become increasingly important for automated inspection. Cameras can capture images of products while software analyzes characteristics such as dimensions, surface appearance, position, shape, or the presence of specific features.
Vision inspection can operate at production-line speeds and can be integrated with conveyors or automated handling equipment. Lighting, camera position, image resolution, and software configuration all influence inspection results.
Artificial Intelligence in Inspection
Artificial intelligence and machine learning are being explored for applications such as visual defect classification, anomaly detection, and pattern recognition. These systems can analyze large collections of images or measurements and identify patterns that may be difficult to evaluate manually.
AI-based inspection still depends on appropriate training data, validation, measurement methods, and human oversight. A digital classification result should be interpreted within the context of the inspection system and its defined acceptance criteria.
Connected Sensors
Industrial Internet of Things technologies allow sensors and equipment to communicate measurement information across production networks. Quality-related measurements can be combined with machine operating data, environmental information, and production records.
This approach can help organizations study relationships between process conditions and product results. It also creates larger volumes of data that need appropriate storage, security, validation, and management.
Automated Measurement
Coordinate measuring machines, laser measurement systems, optical scanners, automated gauges, and other instruments can collect precise dimensional information. Automated measurement reduces repetitive manual recording and can connect inspection results with production databases.
Three-dimensional scanning can also create digital representations of physical components. These models can be compared with defined geometries to identify dimensional differences.
Predictive Quality Monitoring
Quality monitoring is increasingly connected with predictive approaches. Historical measurements can be analyzed to identify trends that may precede process deviations.
For example, gradual changes in machine vibration, temperature, pressure, or dimensional measurements may indicate that a process is changing. Predictive monitoring does not replace physical inspection; it provides another source of information for process management.
Laws or Policies
Industrial quality control systems are influenced by product regulations, industry standards, workplace requirements, environmental rules, measurement standards, and documentation requirements. The applicable framework varies according to the country, industry, product category, and manufacturing process.
Quality Management Standards
Many industrial organizations structure their quality management activities around recognized standards. These frameworks commonly address documented processes, measurement, internal review, corrective actions, traceability, and continual process evaluation.
Quality management standards do not replace product-specific regulations. Instead, they can provide a structured approach for managing quality-related activities.
Measurement and Calibration
Testing equipment needs appropriate calibration and verification when measurements are used to make quality decisions. Calibration establishes a relationship between an instrument's readings and recognized measurement references.
Equipment records can include calibration dates, measurement results, instrument identification, and inspection history. The required calibration approach depends on the instrument and the measurement application.
Product and Industry Requirements
Different industries can have specific requirements for testing and documentation. Automotive components, electrical equipment, construction materials, food products, medical equipment, and aerospace components can all have different quality expectations.
Manufacturers need to identify the applicable requirements for their products rather than assuming that one testing framework applies to every industry.
Workplace Safety
Testing laboratories and production inspection areas can contain electrical equipment, moving machinery, heat, pressure, chemicals, radiation-producing equipment, or other hazards depending on the application.
Safety procedures may address equipment guarding, protective equipment, ventilation, emergency controls, handling procedures, and appropriate training. Requirements vary according to the hazards present.
Tools and Resources
Industrial quality control planning involves several types of technical tools. Measurement equipment provides physical data, while software organizes results and supports statistical analysis.
Statistical process control tools can help users monitor process variation over time. Control charts, capability calculations, sampling plans, and measurement-system analysis can provide structured ways to examine production information.
Useful resources include:
Digital calipers and micrometers
Coordinate measuring machines
Machine vision systems
Optical measurement equipment
Surface measurement instruments
Hardness testing equipment
Ultrasonic testing systems
Statistical process control software
Laboratory information management systems
Manufacturing execution systems
Calibration management platforms
Inspection checklists
A simplified comparison of common quality control technologies is shown below:
| Technology | Primary Purpose | Typical Data |
|---|---|---|
| Machine Vision | Visual inspection | Images and classifications |
| Coordinate Measurement | Dimensional inspection | Position and geometry |
| Ultrasonic Testing | Internal inspection | Wave responses |
| Hardness Testing | Material characteristics | Hardness values |
| Digital Gauges | Dimensional checks | Measurement values |
| Temperature Sensors | Process monitoring | Temperature readings |
| Pressure Sensors | Process monitoring | Pressure readings |
| Statistical Software | Process analysis | Trends and variation |
Statistical Process Control
Statistical process control uses measurements collected during production to examine process variation. Control charts can show whether measurements remain within defined statistical boundaries or display patterns that require investigation.
Process capability analysis can compare observed process variation with specified requirements. These calculations depend on appropriate sampling, stable measurement methods, and correctly defined specifications.
Calibration Management
Calibration management platforms can track inspection instruments, calibration intervals, equipment identification, and historical records. This helps organizations maintain organized information about measurement equipment.
Measurement-system analysis can also be used to examine whether an inspection method produces sufficiently consistent results for its intended application.
FAQs
What are industrial quality control systems?
Industrial quality control systems are organized methods for inspecting materials, measuring production characteristics, identifying deviations, and documenting quality-related information. They can combine testing equipment, sensors, software, procedures, and human inspection.
How does modern testing technology improve quality control?
Modern testing technology can automate measurements, collect data continuously, inspect products using cameras, and connect test results with production records. The actual capabilities depend on the equipment and application.
What is machine vision in industrial quality control?
Machine vision uses cameras, lighting, image-processing software, and defined inspection criteria to examine products or production processes. It can identify selected visual or dimensional characteristics without relying entirely on manual inspection.
How are sensors used in industrial quality control systems?
Sensors measure process conditions such as temperature, pressure, vibration, flow, weight, or position. The information can be recorded and analyzed to identify changes in production conditions.
Why is calibration important for industrial testing equipment?
Calibration helps establish confidence in measurement accuracy by comparing an instrument with an appropriate reference. Calibration records can support traceability and help identify instruments that require adjustment or further examination.
Conclusion
Industrial quality control systems combine inspection, measurement, testing, monitoring, documentation, and analysis to manage variation in manufacturing processes. Modern technology has expanded these systems through machine vision, connected sensors, automated measurement, digital records, and data analysis. Effective quality control depends on suitable measurement methods, defined specifications, equipment calibration, appropriate documentation, and industry-specific requirements. The technology used varies according to the product, manufacturing process, inspection objective, and applicable quality framework.